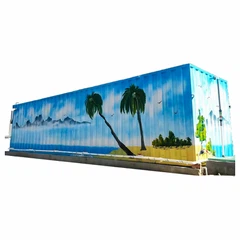
As international cooperation continues to grow, LingKe Environmental Technology recently welcomed a customer from Somalia to inspect a customized containerized reverse osmosis (RO) water treatment system before shipment.
The system was specially designed to support a hotel water supply project in Somalia, providing a compact and integrated solution that can simplify transportation, installation, and future operation.
During the visit, the customer carefully inspected the overall equipment layout, key components, piping arrangement, and electrical control system. Our engineering team introduced the system configuration, answered technical questions, and discussed the project requirements to ensure every detail met the customer's expectations before delivery.

The containerized RO system integrates pretreatment, reverse osmosis, high-pressure pumps, and intelligent electrical controls into one compact unit. Its factory-assembled design helps reduce on-site installation time while making transportation and commissioning more convenient.
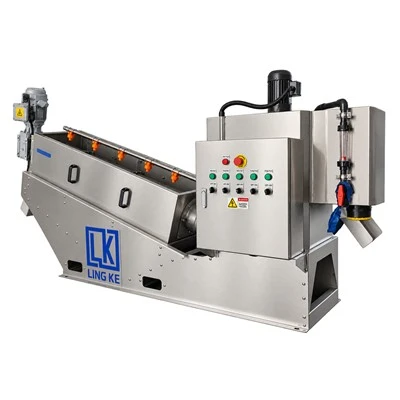
After inspecting the RO system, the customer also toured LingKe's production workshop to learn more about our other water treatment equipment, including packaged sewage treatment systems and reverse osmosis solutions for different commercial and industrial applications. The visit provided a deeper understanding of our manufacturing capabilities and quality control process.

At LingKe Environmental Technology, every project undergoes careful inspection before shipment. From equipment manufact
uring and assembly to factory testing and customer acceptance, we strive to provide reliable water treatment solutions tailored to different application requirements.
We sincerely appreciate our Somali customer's trust and look forward to supporting the successful implementation of this hotel water supply project. LingKe will continue providing customized water treatment solutions for customers around the world.